
Industrial Storage Silos
Falco Latinoamericana designs, engineers, and manufactures industrial silos for mass-flow applications and large-scale bulk material storage. Our solutions are engineered to ensure optimal storage conditions for raw materials and ingredients across the food, chemical, pharmaceutical, and cosmetics industries.

Vertical Storage Solutions with Reliable Structural Integrity
Bulk material storage requires a thorough analysis of product flow properties, including bulk density, angle of repose, and flowability.
At Falco, we develop vertical storage silos engineered in accordance with international mechanical design and safety standards. Our designs minimize the risk of material segregation, compaction, and stagnant flow zones, ensuring consistent, safe, and efficient discharge while protecting the quality and value of stored raw materials.
Engineering Advantages of Falco Industrial Silos
Optimized Discharge Geometries
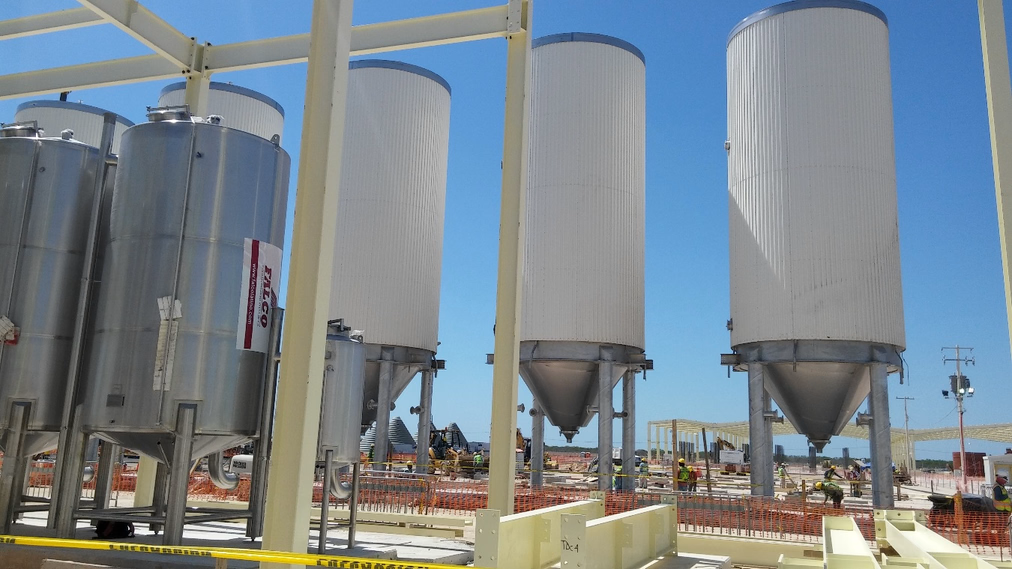
We design conical bottoms, flat bottoms, and specialized hopper transitions with engineered discharge angles to prevent common flow problems such as ratholing and material bridging.
Superior Sanitary and Hygienic Design
Our silos feature mirror-polished interior welds and smooth, crevice-free surfaces designed to support compliance with applicable FDA and COFEPRIS sanitary requirements for food and pharmaceutical applications.
Thermal Insulation and Jacketed Systems
Available with heating or cooling jackets and high-density injected polyurethane insulation, protected by stainless steel exterior cladding for precise temperature control.
Engineered Structural Support Systems
Our anchoring systems, continuous support skirts, and structural legs are mechanically engineered to withstand dynamic loads, high wind forces, and seismic conditions based on the installation site's geographic location.
Precision Metallurgy and Integrated Instrumentation
We manufacture our industrial silos using 304, 304L, 316, and 316L stainless steel.
Each silo can be equipped with advanced industrial instrumentation, including load cells for real-time weighing, continuous level sensors (radar, ultrasonic, or capacitive), dust collection vent filters, pressure/vacuum relief valves, and hermetically sealed inspection hatches.
Applications in Large-Scale Industrial Processing
Sanitary Storage of Food Ingredients and Products
Silos designed for the storage of food-grade powders and liquids, including milk, juices, flour, sugar, starch, and oils.
High-quality interior polishing helps minimize bacterial growth and facilitates automated Clean-in-Place (CIP) cleaning cycles.
Chemical Raw Material and Plastic Resin Storage
Heavy-duty storage systems for resins, plastic pellets, chemical additives, and corrosive fluids. Designed with engineered wall thicknesses and protective coatings to minimize wear caused by abrasion and aggressive chemical corrosion.
Integration with Pneumatic and Mechanical Conveying Systems
Our silos serve as the central storage units in automated material handling and transfer systems. They can be seamlessly integrated with screw feeders, rotary discharge valves, vibrating bin dischargers, and dense-phase or dilute-phase pneumatic conveying lines.
Types of Industrial Silos
Vertical Tower Silos
- These tall, cylindrical structures are typically manufactured from stainless steel.
- They maximize vertical space, provide high storage capacity, and allow efficient gravity discharge.
- Their installation requires a solid foundation to ensure structural stability.
- Vertical tower silos are widely used for storing grains, cement, minerals, and other bulk materials across multiple industries.
Metal Silos (Stainless Steel or Carbon Steel)
- Metal silos are robust, durable, and designed to withstand demanding industrial operating conditions.
- Stainless steel configurations offer excellent corrosion resistance and ease of cleaning, making them suitable for applications with strict hygiene or chemical compatibility requirements.
- Although their initial cost may be higher than that of alternative materials, their long service life makes them a reliable investment.
- They are commonly used in the chemical, food, pharmaceutical, and materials processing industries.